

Alfa Laval launches new MaxiLobe rotary lobe pumps for higher efficiency and uptime, with lower total cost of ownership
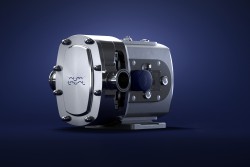
/INS. Alfa Laval is introducing the MaxiLobe rotary lobe pump ranges, new positive displacement pumps designed to improve volumetric efficiency, with the potential to reduce capital investment and deliver energy savings. They also extend the operating range while protecting product quality, simplifying maintenance and increasing uptime in hygienic and high-purity applications.
Kolding, Denmark, October 2026
A higher standard for demanding hygienic processes
Manufacturers in the dairy, food, beverage, home and personal care, and pharmaceutical industries are under constant pressure to improve efficiency, maximize uptime and reduce the total cost of ownership. The Alfa Laval MaxiLobe and MaxiLobe UltraPure pump ranges address these priorities through higher volumetric efficiency, a broader operating envelope, enhanced assurance and simpler service.
“For decades, our rotary lobe pumps have been widely used in hygienic and high-purity processing where reliability and predictable performance are essential,” says Russ Kelly, Portfolio Manager, Pumps at Alfa Laval. “MaxiLobe builds on that legacy with improved hygienic design across a wider operating range, enabling smaller pumps to achieve the same duty at lower speeds. Lower speeds reduce shear, helping improve operating efficiency and safeguard shear-sensitive products.”
Optimized investment
MaxiLobe and MaxiLobe UltraPure pumps help optimize capital investment through high volumetric efficiency and an exceptionally broad flow and pressure envelope. Additionally, by enabling a smaller pump to be selected for the required duty in suitable applications, MaxiLobe can reduce equipment and installation costs, including the associated electrical equipment. This reduces the need for oversizing while maintaining operational flexibility.
Upgrades are equally straightforward. Key porting dimensions match those of all Alfa Laval SRU pumps and most SX and SX UltraPure models, allowing replacement without modifying existing pipework. Under defined operating conditions, MaxiLobe delivers at least 5% higher flow rates than the equivalent SRU model, improving process capacity without increasing footprint or installation complexity.
Cost-effective operation
MaxiLobe and MaxiLobe UltraPure pumps can deliver the required flow rates at lower operating speeds, helping reduce energy consumption and electricity costs. In many applications, this can result in energy savings of more than 25%. Operating the pumps at lower speeds also reduces shear on sensitive products that may be damaged when operating at higher speeds. By reducing mechanical stress, MaxiLobe pumps can help extend service intervals and equipment life.
A robust gearbox design supports reliable performance under demanding conditions, reducing the risk of unplanned stoppages and supporting more predictable, resource-efficient operation and lower lifecycle costs.
Enhanced assurance
MaxiLobe and MaxiLobe UltraPure pumps protect product quality and reduce cross-contamination risk through precision-profiled elastomers, superior cleanability and hygienic and high-purity design. MaxiLobe provides both EHEDG and 3-A certification alongside full FDA compliance as standard, delivering an uncompromised hygienic solution.
For pharmaceutical and biotech applications, MaxiLobe UltraPure complies with ASME BPE standards and Good Manufacturing Practices guidelines. It offers material options, enhanced surface finishes and product-wetted materials conforming to FDA and USP requirements. Comprehensive Alfa Laval Q-doc documentation provides full traceability and validation support for use in regulated manufacturing environments.
Every pump is factory-tested and supplied with a performance certificate confirming that it meets its specified operating curve before delivery, ensuring reliable commissioning and smooth start-up.
Simpler service
MaxiLobe and MaxiLobe UltraPure are engineered for quick, predictable maintenance. Front-loading single seals can be replaced without removing the pump from the process line, reducing downtime during routine service. Interchangeable components and easily accessible shimming simplify servicing and help reduce maintenance time. Alfa Laval’s global service organization further supports maintenance wherever the pumps are installed.
To learn more, visit Alfa Laval MaxiLobe and Alfa Laval MaxiLobe UltraPure.
For further information, please contact:
Russ Kelly
Portfolio Manager, Pumps
Alfa Laval
E-mail: russ.kelly@alfalaval.com
This is Alfa Laval
Working closely with customers and partners worldwide, Alfa Laval challenges conventional thinking on engineering, quality, and innovation. Together driving the solutions of the future, inspiring progress towards a more resourceful, less wasteful world.
Alfa Laval is set on creating positive impact in areas that society depends on, including energy, food, water, medicine, maritime transport and offshore operations. As a leading global provider of solutions in heat transfer, separation, and fluid handling, the company collaborates closely with many industries to optimize efficiency, reduce emissions and increase yields.
Alfa Laval was founded more than 140 years ago, has customers in over 100 countries, employs more than 23,500 people, and annual sales were 69.6 BSEK (6.6 BEUR) in 2025. The company is listed on Nasdaq Stockholm.

 Vector graphic
Let us know if you are going to use this press release. Thank you!